Hot Dip Galvanized Bolts Manufacturer: HDG Bolts, Nuts and Washers for Outdoor Structures
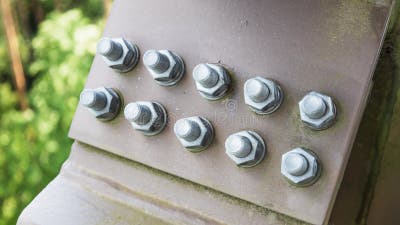
WF Fastener is a hot dip galvanized bolts manufacturer and supplier for outdoor structures and power infrastructure projects across Asia, Europe and the Middle East, producing hot dip galvanized structural bolts, transmission tower bolts, lattice tower fasteners and HDG nut-washer assemblies for transmission towers, substation structures and general outdoor steelwork, according to ISO 10684 coating requirements and project specifications. Our galvanizing line controls coating thickness and uniformity to ISO 10684, and every lot ships with coating thickness verification, material certification and EN 10204 3.1 documentation.
WF Fastener — HDG Bolts Quick Reference:
- Products: HDG hex bolts, HDG nuts, HDG washers, anchor bolts and stud bolts for outdoor structures
- Coating: hot-dip galvanizing per ISO 10684, with coating thickness matched to service environment
- Materials: structural carbon steel, property classes matched to the application (e.g. 4.6, 5.6, 8.8 where specified)
- Threading: nut over-tapping per ISO 965-5 (6AZ / 6G thread allowances), thread inspection after galvanizing
- Grid standards: EN 50341 overhead line towers and DIN 7990 tower bolts referenced where the project specifies
- Testing: coating thickness verification, adhesion checks, hardness verification, material certificates
- Standards: ISO 10684 / ISO 4014 / ISO 4032 systems, EN 10204 3.1 material certificates
What Hot-Dip Galvanizing Does
Hot-dip galvanizing protects outdoor structural bolts by immersing clean steel into a bath of molten zinc at 450–480 °C, forming metallurgically bonded zinc-iron alloy layers topped by a pure zinc outer layer, protecting the steel by both barrier and cathodic (sacrificial) action. For transmission towers and substation gantries exposed to ISO 12944-2 C3 / C4 / C5 environments, ISO 10684 HDG provides long-term protection. Unlike structural steel beam galvanizing, fastener galvanizing requires automated high-speed centrifuging (spinning) immediately after removal from the zinc bath, which expels excess zinc from the thread roots so the nut assembles over the coated thread. The coating thickness is typically several times that of electroplating; typical HDG coating thickness requirements under ISO 10684 are approximately 40–85 µm depending on fastener diameter.
For a procurement engineer, the key specification points are the coating thickness (matched to the environment and the design life), the thread fit (nuts must be over-tapped so they assemble over the coated thread), and the property class (the galvanizing process must not compromise the fastener strength). All three are controlled in our production and documented in the certificate package.
HDG Fastener Types
| Fastener | Typical Use | Key Points |
|---|---|---|
| HDG hex bolts | General outdoor steelwork, substations, lattice structures | ISO 10684 coating, thread fit after galvanizing |
| HDG nuts | Matching the coated bolt thread | Over-tapped per ISO 965-5 (6AZ), hardness matched to bolt class |
| HDG washers | Load distribution under the nut and head | Coating on all surfaces, hole size per the bolt |
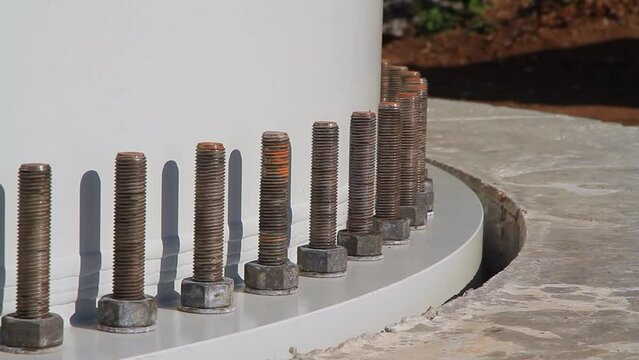
| HDG anchor bolts | Foundation connections for structures | Long bolts, coating thickness over full length, embedment documentation |
| HDG stud bolts | Flange and structural connections | Thread inspection after galvanizing, nut fit verification |
Materials and Property Classes
- Structural carbon steel — property classes are selected according to the structural design requirement, commonly including 5.8 and 8.8 for galvanized structural applications, with other grades available according to project specification, subject to galvanizing compatibility
- Grade verification — hardness and tensile verification per lot, confirming the property class after processing
- Coating thickness — verified per ISO 10684, with minimum thickness matched to the service environment and design life
HDG Bolt Specification Guide
| Specification | Typical Requirement |
|---|---|
| Diameter / length | M6–M64, per the structure drawing |
| Property class | 5.8 / 8.8 for galvanized structural applications, per design |
| Coating | ISO 10684, minimum thickness 40–85 µm by size |
| Thread allowance | Nuts over-tapped for coating, assembly verified |
| Certification | EN 10204 3.1 material certificate, coating thickness report |
What the Buyer Should Specify
A correct HDG fasteners order states: the fastener type and size, the property class, the coating requirement (ISO 10684 with minimum thickness and the ISO 12944-2 environment class, e.g. C3 / C4 / C5), and the certificate scope. For structures where the design references a specific structural bolting system, the bolts, nuts and washers are supplied as a complete set to the referenced system. When the project specifies a higher strength class, our engineering team confirms the galvanizing compatibility before production, because the galvanizing process affects the thread and the fastener properties.
Manufacturing and Quality Control
- Galvanizing — hot-dip galvanizing per ISO 10684 with controlled bath parameters, followed by high-speed centrifuging to clear zinc from the thread roots, giving a uniform zinc-iron alloy coating
- Hydrogen embrittlement control — for 8.8 and above, acid pickling time is controlled and hydrogen removal (baking) is performed where required before galvanizing, per the project requirement
- Coating thickness verification — measured per lot with magnetic gauges, reported in the certificate package
- Thread fit control — nuts over-tapped for the coating allowance; thread inspection after galvanizing confirms assembly with the coated bolt
- Adhesion checks — coating adhesion verified by hammer and knife tests where specified
- Hardness verification — per-lot hardness testing on finished parts, confirming the property class
- Material certificates — EN 10204 3.1 documentation with heat number traceability
Why Buyers Choose WF Fastener for HDG Bolts
- ISO 10684 coating control — coating thickness and uniformity verified according to the agreed inspection plan, with results recorded in the certificate package
- Thread fit assurance — over-tapped nuts and post-galvanizing thread inspection, so the bolt and nut assembly meets the specified installation requirements
- Complete sets — HDG bolts, nuts and washers supplied together with matched coating and hardness
- Full documentation — EN 10204 3.1 material certificates, coating thickness reports and lot traceability
- Project experience — HDG fasteners supplied for transmission, substation and outdoor steelwork projects across Asia and the Middle East
Sourcing and Lead Times
- Common sizes of HDG bolts, nuts and washers are available for dispatch from stock or short production runs, typically 2–3 weeks
- Anchor bolts and project-specific sizes are manufactured to order, typically 3–4 weeks depending on length
- Quotations include the material certification and coating scope, so the commercial offer matches the delivered documentation
FAQ
Q: What is the difference between hot-dip galvanized and electroplated bolts?
A: Hot-dip galvanizing applies a thick zinc-iron alloy coating in a molten zinc bath at about 450 °C, giving long-term outdoor corrosion protection through both barrier and sacrificial action. Electroplating applies a much thinner zinc layer and is used where dimensional tolerance and appearance matter more than coating life. For outdoor structures with long design lives, HDG is the standard choice.
Q: What coating thickness should I specify?
A: ISO 10684 defines minimum coating thickness by thread size, typically 40–85 µm depending on the bolt size. For aggressive environments or longer design life, a thicker coating is specified. Our certificate package reports the measured thickness per lot.
Q: Why are HDG nuts over-tapped?
A: Because hot-dip galvanizing adds 40–85 µm of zinc to external bolt threads, standard nuts will not assemble onto coated bolts. HDG nuts are over-tapped post-galvanizing to ISO 965-5 class 6AZ tolerance (or 6G undercut before coating), ensuring smooth assembly while maintaining full proof-load capacity. Nuts and bolts are supplied as a matched set.
Q: Can HDG be applied to high strength bolts?
A: High strength fasteners such as property class 10.9 require special evaluation before hot-dip galvanizing, because the galvanizing process temperature may affect the tempered structure and acid pickling introduces hydrogen embrittlement considerations. Zinc flake systems are commonly selected for these applications. For 8.8 and below, galvanizing compatibility is confirmed before production.
Q: Do you provide EN 10204 3.1 material certificates?
A: Yes. EN 10204 3.1 certificates are prepared from our in-house testing laboratory and quality documentation system, with heat number traceability available where required.
Q: What is the minimum order quantity?
A: Common sizes start from about 5,000–20,000 pieces depending on type and size, with project-specific sizes quoted by requirement. Send the specification and our team will confirm the MOQ and lead time within one working day.
Request a quote for your HDG fasteners package: send the BOM, tower or structure drawing, coating specification, property class and certificate scope, and our engineering team will confirm the specification and delivery plan within one working day.
📄 Download the HDG fasteners RFQ checklist — type, size, grade, coating thickness and certification requirements, including the ISO 965-5 thread allowance and clearance table for RFQ verification.
📦 Request sample kits — evaluate coating quality, thread fit and assembly behavior before ordering.
💬 WhatsApp engineering support — send the BOM or project inquiry directly to our team.